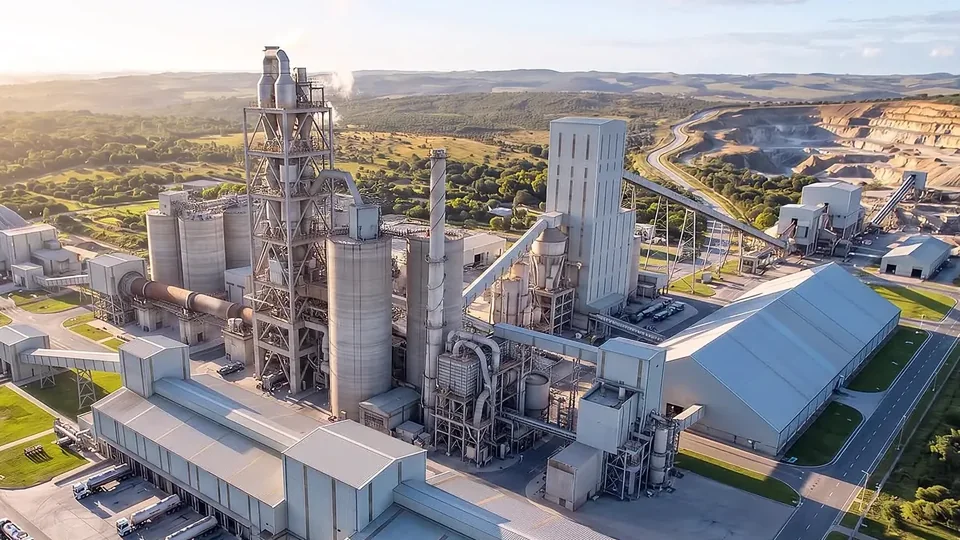
Kiln run factor is the share of all the hours in a period, usually a year, in which the kiln is actually running on feed. Planned shutdown hours count against it, and so does every unplanned stop. Because the kiln sets the pace for the whole plant, the run factor, together with the kiln's daily output, decides how much clinker a plant makes in a year.
Most of the attention goes to the annual shutdown: the refractory, the big mechanical jobs, the days it takes to cool down and heat up. That matters. But a large part of the run factor is decided between shutdowns, in ordinary weeks, by stops that nobody planned.
Where the hours go
- The kiln itself. The girth gear, the tyres and the shell fail slowly and expensively. They are also the items a calendar-based plan tends to cover least well, because they do not fit a monthly routine.
- The mills. A raw mill or finish mill that trips on vibration comes back on line in minutes or hours, so each stop looks small. Repeated week after week, raw mill trips eat into kiln feed stock and, in the end, kiln hours; finish mill trips eat into cement output.
- Conveyors and air slides. A little dust at a joint, some spillage under a belt. Each is a small defect that somebody has walked past. Left alone, small leaks and spillage grow into stops.
Process upsets, such as cyclone blockages, build-ups and brick failures, take their share too. The three above are the mechanical losses that a better maintenance routine can reach.
None of these is dramatic on the day. That is exactly why they persist.
Four habits that protect the run factor
1. See yesterday before 8 a.m. Clinker and cement against plan, kiln run factor and energy per tonne should be on one board before the morning meeting. If the kiln missed its plan yesterday, the first question of the day is who owns that miss, not whether the number is right.
2. Prove the cause before you close the job. A trip that stopped without anyone finding the cause will come back. Test the likely causes one at a time, record what each test showed, and treat the job as fixed only when the machine has run a fair test without the fault.
3. Tag the small things. Give every operator and technician a simple way to report a dust leak, a missing guard or spillage, and make sure each report reaches a named person with a date. Close it only when there is proof.
4. Plan the shutdown from the failures. The best shutdown scope comes from what actually failed and what was found during the year, not from repeating last year's list.
The point
Kiln run factor is made on the shift, not in the shutdown. A long shutdown list does not hold a high run factor by itself. What holds it is seeing every miss the next morning, proving the cause, and putting what was learned into the plan.
How EXLATECH helps: see the four apps set up for cement, from a daily run-factor board to an RCM programme for the kiln and mills. Book a demo.