Pipes
OEE in metres, not kilograms.
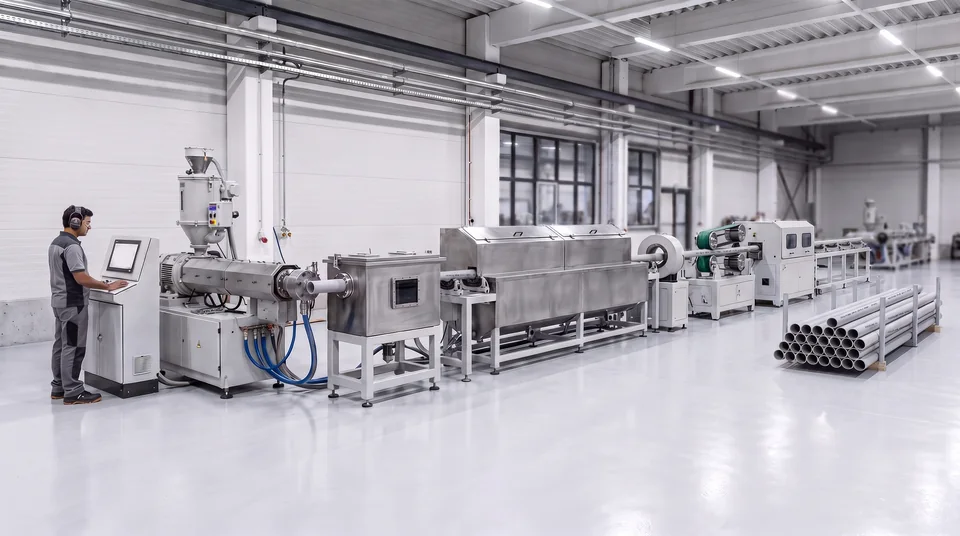
HDPE and PVC pipe line efficiency: less start-up scrap, shorter die changes, and extrusion line downtime caught on day one.
Where the losses hide
Where an extrusion line loses metres.
Extruders and heaters
Heater zones that fail quietly, and wall thickness that swings.
Die changes and start-ups
Die change time and the scrap of every start-up.
Cooling and cutting
Vacuum tanks, haul-offs and saws that stop the line.
Four apps, set up for pipes.
Extrusion line maintenance from the failures, down to the high melt-pressure shutdown nobody tested.
For pipes →
Scrap for wall thickness and metres against plan on one board, before 8 a.m.
For pipes →
Walls swinging thick then thin: the resin ruled out, the failing heater zone proven.
For pipes →
A few drops at a hydraulic hose fitting: tagged, fixed and closed with the after photo.
For pipes →
The engineering intelligence built into every OPEX Suite app, working alongside your engineers. They stay in charge of every decision.
One case, start to finish
Line 2 scrapped pipe for wall thickness.
- 01
Caught on day one
The scrap is on the Plant screen by 6:30, owned before 8 a.m. and sent to EDPS.
- 02
The cause, proven
Everyone blamed the new resin lot. EDPS ruled it out; the check proved heater zone 3.
- 03
Fixed, by the clock
A new heater band, proven over the test period. Two days later Line 2 was back on plan.
- 04
In the plan
The shutdown that stops the extruder on high melt pressure had never been tested. Now it is.
Advice as well as software
Need help on the floor too?
TPM and operational excellence consulting with your own team: see how we work with plants.
Other industries
Bring one machine that keeps stopping.
In a 30-minute demo, we'll show you how the four apps handle it, from the first tag to the fix that stays.